
Which is better for a high-volume PET bottle plant: a specialized mold maker or a full-line equipment supplier?
Choose a specialist mold maker for a defined tooling task or a full-line supplier for coordinated equipment scope, with clear ownership of every interface.
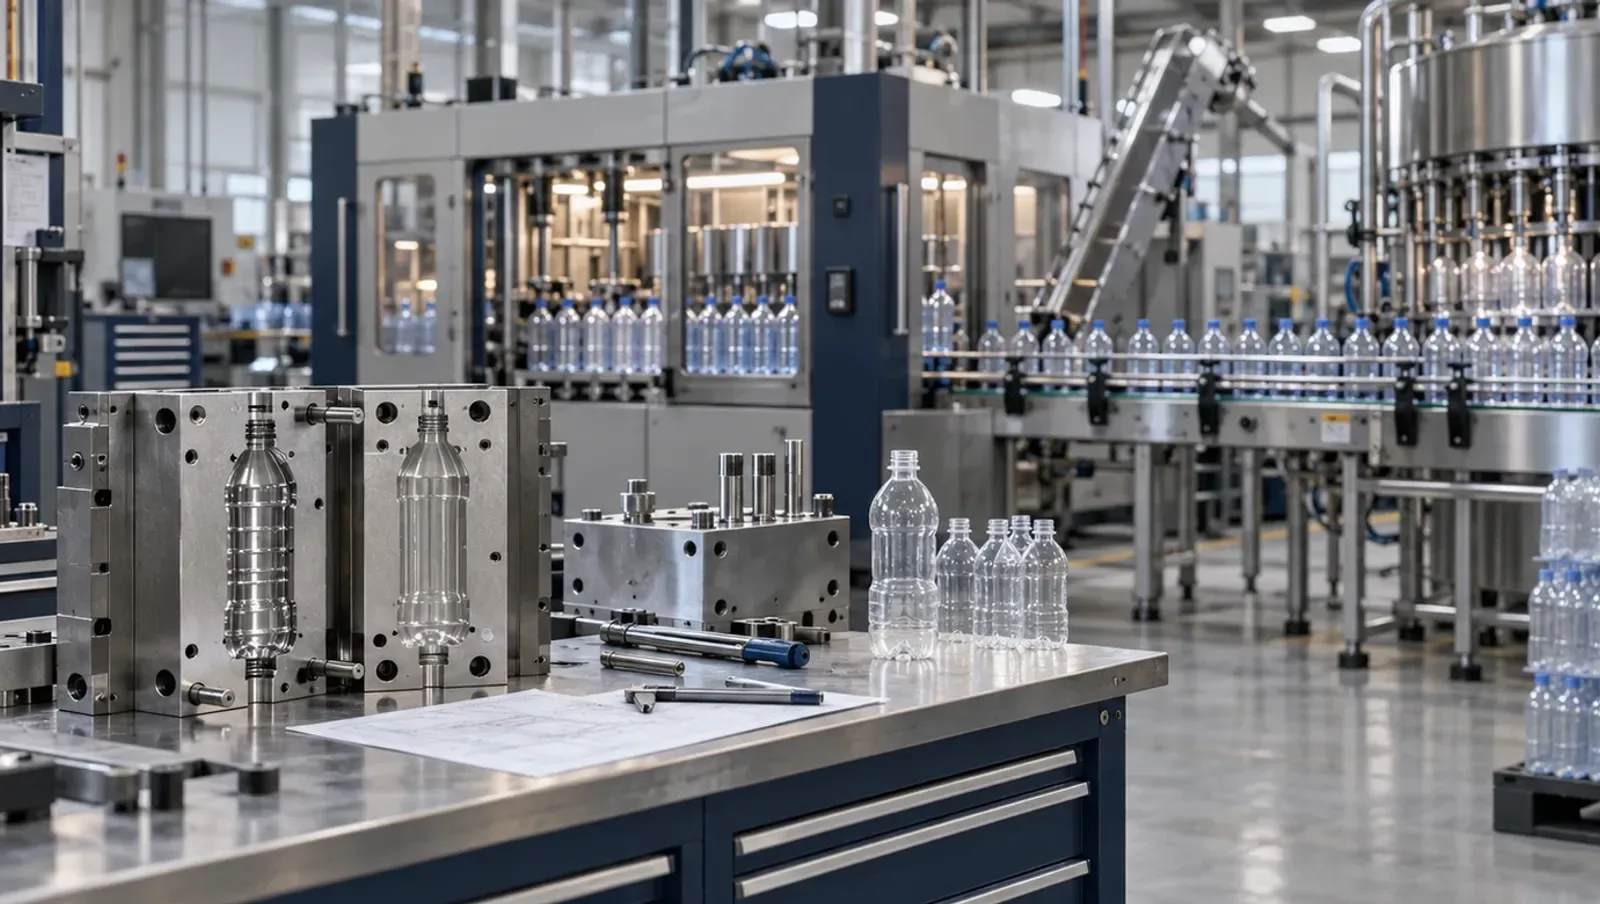
Choose by project boundary and integration responsibility
A specialized mold maker supplies tooling and related engineering; a full-line equipment supplier coordinates a broader set of production equipment within its quoted scope. A specialist is a sensible route for a defined mold replacement or conversion on an established line, while a full-line proposal deserves consideration for a new plant or extensive equipment changes. The better choice depends on who owns integration, qualification and service across the required process.
Compare the actual scope, not the supplier category
| Dimension | Specialist tooling route | Full-line route |
|---|---|---|
| Core task | A defined mold or component project | A coordinated equipment project |
| Installed machines | Interfaces must be confirmed | Included machine scope must be confirmed |
| Bottle design | Agree development and tests | Agree packaging development and tests |
| Integration | Plant or named integrator coordinates | Confirm contracted integration boundary |
| Utilities | Plant documents actual available conditions | Supplier and plant agree equipment requirements |
| Commissioning | Mold and related interface acceptance | Equipment and line acceptance |
| Service | Tooling and parts responsibilities | Check line and individual equipment support |
| Commercial comparison | Engineering, tooling and downtime | Equipment, integration and qualification |
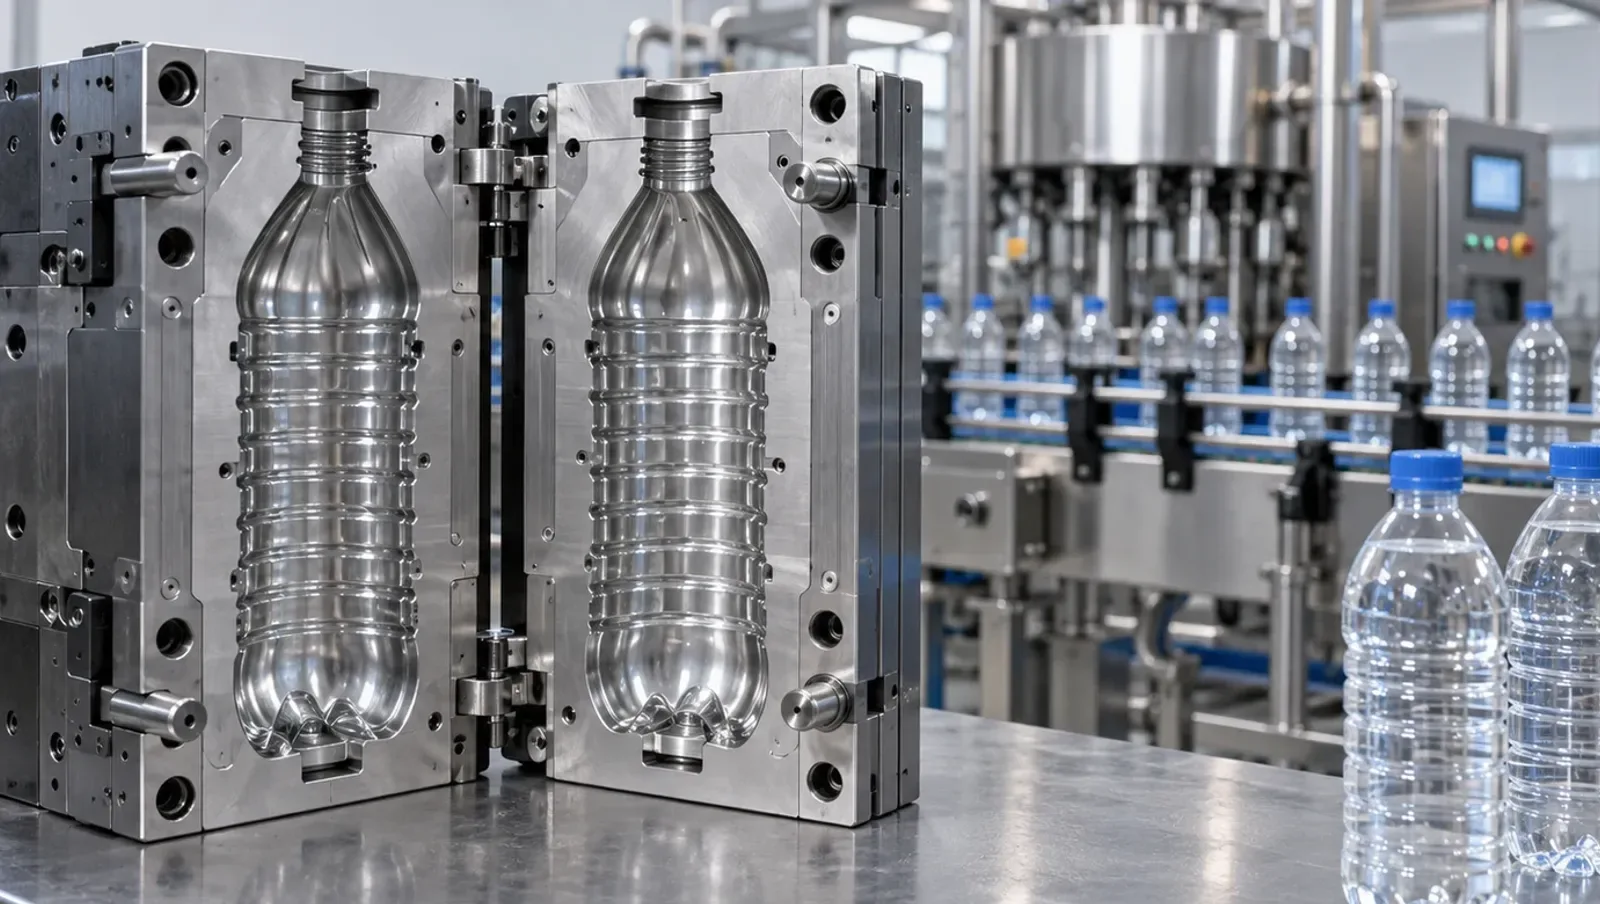
Neutral examples of different supplier roles
- Otto Hofstetter publishes PET preform moulds. It is an example of a specialist tooling offering to investigate. Compare the specific tool, machine interface and service arrangements rather than treating specialization as proof of better quality or lower cost.
- Sidel publishes complete water bottling lines. Its offering is relevant when the purchase includes coordinated bottle-production equipment. The quoted line boundary still needs review: upstream preform manufacture, utilities and individual package-development tasks should not be assumed to be included.
- SIPA publishes preform tooling and conversions, and Husky publishes integrated injection systems and hot runners. These illustrate why a procurement decision may involve both tooling and upstream equipment, even before the blowing and filling equipment is considered.
- LIHE publishes molds, hot runners, components and tooling conversion. That scope is useful to evaluate for an established-machine project. LIHE should not be presented as a substitute for every machine and complete-line contractor; agree its responsibilities with the plant and equipment suppliers.
Decide using the plant’s actual operating situation
- For a stable line needing a replacement preform mold, begin with the machine and package specification already approved. A bounded tooling project can preserve established equipment while changing the mold. Check whether the proposed conversion also affects cooling, controls, handling or closure geometry.
- For a new plant, map the whole process from preform supply to finished package. Decide whether injection is on site, then identify blowing, filling, capping and transport responsibilities. A complete-line proposal can coordinate more equipment, but only the contracted scope establishes that responsibility.
- For simultaneous lightweighting and equipment changes, appoint an engineering owner for the package. Freeze the preform, bottle and closure requirements and sequence the trials. Neither supplier category removes the need to test the final bottle or resolve changes between the injection and blowing stages.
- Use a specialist when the plant or its integrator can manage the interfaces; consider a broader equipment contractor when that coordination is part of the purchase requirement. Where responsibility remains unclear, resolve it before awarding the job instead of relying on the supplier’s category name.
Split acceptance between the mold maker and the line supplier
- Step 1: Draw up an interface responsibility matrix before any purchase order. List each physical and data interface, such as platen and hot half, cooling water, controller signals, take-out robot, conveyor and blow molder infeed, and give every row one named owner and one approver.
- Step 2: Hold a factory acceptance test for the mold at the mold maker's site. The mold maker owns this test: dimensions per cavity, hot-runner heating and valve-gate function, cooling-circuit flow and a stable molding run on a comparable machine. Sign it off as a mold result, not as a line result.
- Step 3: Hold the equipment acceptance with the line supplier for the machines it contracted. The line supplier demonstrates speeds, changeovers and controls for its own scope; ask it to state in writing which upstream inputs, including preforms, it assumed for that test.
- Step 4: Run a joint site acceptance with both parties present once the mold is installed on the plant's machine and connected to the downstream line. Agree in advance how defects are attributed: a preform out of tolerance points to mold or injection settings, while a bottle defect from a conforming preform points to blowing or line settings.
- Step 5: Close the project with a handover file from each party and one shared open-items list. Each open item carries an owner and a date, so that nothing falls into the gap between the tooling contract and the equipment contract.
After start-up: who services what
- Mold wear parts, including neck rings, cores, cavities, nozzle tips and valve pins, normally come from the mold maker or a qualified tooling source. Machine wear parts come from the machine builder. Keep the two spare-parts lists separate so a stock-out is traced to the right supplier.
- With a full-line contract, the plant usually has one commercial contact, but the line supplier may still pass a tooling problem to its own mold subcontractor. Ask who actually performs mold repairs, where they are done and how long the tool is out of production when it leaves the site.
- With a specialist route, the plant or its integrator coordinates between suppliers. That gives direct access to the people who designed the tool, but it also means the plant's engineers must recognize whether a fault starts in the mold, the machine or the downstream equipment.
- Decide where refurbishment happens before the first major overhaul is due. Some work can be done on site; hot-runner and cavity refurbishment often needs the tool at the maker's workshop. Plan a spare mold set or an alternative supply of preforms for that period.
- Write the service expectations into each contract: remote support channels, on-site visit terms, spare-parts lead times and how revised drawings are distributed. A line contract and a tooling contract that describe service in different terms make cross-supplier faults slower to solve.
Where LIHE sits in this choice
This guide comes from LIHE Precision, a specialist tooling supplier rather than a full-line contractor, so read it with that position in mind. The figures below are published on lihe-preform.com and describe the tooling side of the decision only; line equipment, integration and overall line acceptance remain with the plant or its equipment suppliers.
- Tooling range: PET preform molds of 32 to 160 cavities for HUSKY, NETSTAL, SIPA, KATA and other machines, plus valve-gate hot runners up to 144 cavities for preforms, sold with a 3-year leakage-proof guarantee on the Husky Ultra-type design.
- Compatibility with installed equipment: conversion parts are published as 100% interchangeable for Husky, SACMI, SIPA, NETSTAL, MHT, OTTO, ASB, Krupps and Corvaglia systems. That is relevant when the plant keeps its machines and only changes tooling.
- Lead times for the tooling share of a project: pilot molds 20 days, standard PET preform and blow molds 8 weeks, replacement parts 4 weeks. Line equipment schedules sit outside these figures and should be planned with the line supplier.
- Service on the tooling side: machine interface audits, mold installation, machine start-up support, preventive maintenance, remote troubleshooting, spare parts and mold refurbishment. Agree the exact package in the quotation and map it onto the responsibility matrix above.
Frequently asked questions
- Is a complete-line supplier always better for high volume?
- No. High volume describes production demand, not the scope of the purchase. A defined mold replacement and a new complete plant need different responsibilities and acceptance evidence.
- Can a specialist supplier support a large plant?
- Evaluate the specific tooling and service proposal. Confirm the machine interfaces, qualification plan and parts arrangements. Supplier category alone does not establish whether the project meets the plant’s production requirement.
- Does a complete water line include preform injection?
- Do not assume that. The plant may buy preforms or operate separate injection equipment. Ask the line supplier to identify exactly where its contracted scope begins and ends.
- Who should own a cross-supplier defect?
- Name an integration owner before ordering and agree how mold, machine and package issues will be investigated. Maintain one approved package specification and a record of design changes across the suppliers.
References
Related products
Have a mold project? Our engineers can review your requirements.
Request a Quote